Large-format water systems
5 Gallon Water Filling Lines from China
Define returnable-bottle handling, internal and external washing, filling, capping, inspection and finished-bottle movement around the local distribution model.
Published by Allot Tech. Project contact: founder Mr Kcal. Final engineering, performance, materials, compliance, manufacturing responsibility and commercial terms must be confirmed for the selected resource and signed project scope.
Updated September 3, 2026
Direct answer
The bottle-return and sanitation model shapes the complete 5 gallon line.
A 5 gallon project is not simply a larger version of a small PET line. Returnable containers may arrive with labels, caps, dirt, odor or damage, and their washing sequence, inspection and rejection rules affect hygiene and output. The buyer should also define whether bottles are manually loaded, automatically conveyed, bagged, racked or handled by local delivery staff.
Project definition
Start with the complete decision basis.
A 5 gallon project is not simply a larger version of a small PET line. Returnable containers may arrive with labels, caps, dirt, odor or damage, and their washing sequence, inspection and rejection rules affect hygiene and output. The buyer should also define whether bottles are manually loaded, automatically conveyed, bagged, racked or handled by local delivery staff.
Bottle loop
Returnable or new bottle policy, 3 or 5 gallon sizes, bottle condition and daily return pattern.
Sanitation
Pre-inspection, decapping, external wash, internal wash stages, chemicals, rinse quality and verification.
Output
Target bottles per hour, operating shifts, manual labor plan and finished-bottle storage.
Distribution
Cap and label, bag or sleeve, rack use, loading method and local route requirements.
System or development path
Treat returned-container control as part of the production line.
Bottle receiving
Define unloading, sorting, storage and separation of damaged or unsuitable returned bottles.
Decapping and pre-wash
Remove closures and visible contamination before the main washing sequence.
Internal and external washing
Confirm wash stages, chemicals, temperature, contact time, rinsing and drainage.
Inspection and filling
Set rejection points, treated-water connection, filling method and hygiene controls.
Capping and coding
Match cap sanitation, application, tamper evidence, coding and visual checks.
Bagging, racks and dispatch
Plan finished-bottle protection, rack handling, warehouse flow and route loading.
Quotation comparison
Compare 5 gallon lines using the same bottle-condition assumptions.
| Decision area | Buyer should provide | Proposal should clarify |
|---|---|---|
| Returned bottles | Bottle material, sizes, typical contamination and rejection policy. | Inspection, decapping and wash design assumptions. |
| Wash sequence | Buyer hygiene requirement and available chemicals. | Stages, tanks, heaters, dosing, contact time, rinses and monitoring. |
| Labor | Manual loading, inspection, rack handling and dispatch plan. | Automation boundary, operator stations, safety and realistic output. |
| Factory flow | Dirty-bottle entry and clean finished-bottle exit. | Separation, drainage, floor space, access and storage. |
| Verification | Wash and product-quality checks required by the buyer. | FAT basis, records and tests that require qualified local or laboratory review. |
Solve the next project problem
Close these proposal gaps before price becomes the decision.
Use the brief below to turn a vague supplier conversation into questions that can be answered and documented.
Make this decision comparable.
Send: Bottle material, sizes, typical contamination and rejection policy.
Require: Inspection, decapping and wash design assumptions.
Make this decision comparable.
Send: Buyer hygiene requirement and available chemicals.
Require: Stages, tanks, heaters, dosing, contact time, rinses and monitoring.
Make this decision comparable.
Send: Manual loading, inspection, rack handling and dispatch plan.
Require: Automation boundary, operator stations, safety and realistic output.
Send the beverage, package files, required output, factory conditions, destination and current project stage. The Allot Tech Project Desk can help organize the first comparison.
Decision evidence
Keep project evidence connected to each approval and release decision.
Evidence should be identified before the order or approval stage so both sides know what will support the next decision.
Approved engineering basis
Keep the signed specification, equipment list, package files, layout and interface responsibilities under revision control.
Manufacturing progress record
Identify agreed drawings, component confirmations, photographs, open questions and approval decisions by date.
Test and acceptance record
State configuration, materials, operating conditions, measurements, results, punch-list items and release status.
Delivery and handover package
Connect packing, serial numbers, manuals, backups, spare parts, training and support contacts to the delivered scope.
Separate dirty and clean flow
Layout should reduce cross-traffic between returned bottles, washing, filling and finished-bottle storage. Drainage, chemical handling, ventilation and operator access deserve the same attention as machine footprint.
- Map bottle and personnel movement
- Reserve wash-water drainage
- Identify chemical storage responsibility
Output depends on bottle condition
Badly contaminated, damaged or mixed bottles slow sorting and washing. A reliable capacity discussion should state the input-bottle condition and the manual tasks included in the operating basis.
- Define rejection criteria
- Record manual inspection points
- Avoid quoting only theoretical cycles
Confirm sanitation responsibility
Equipment can support a defined washing process, but local water regulations, chemical validation, microbiological checks and operating procedures remain with qualified project parties.
- Agree wash recipe inputs
- Define rinse-water quality
- Plan verification and recordkeeping
Decision gates
Move forward when the next commitment has enough written evidence.
Project stages overlap, but each commercial commitment should have a visible basis, named approvers and a list of unresolved items.
Engineering basis approved
The product, package, output, equipment boundary, layout, utilities, responsibilities and open assumptions are controlled.
Manufacturing and test basis approved
Drawings, component schedule, test materials, acceptance conditions, documents and planned evidence are agreed.
Delivery and handover released
Punch-list closure, packing, shipment files, site readiness, installation scope, training and support ownership are visible.
Before requesting a proposal
Build one brief that every resource can answer on the same basis.
This page is designed to help an international buyer prepare a clearer discussion, not to replace the responsible resource’s engineering or the buyer’s professional review.
Product
Beverage, process, hygiene, shelf-life and operating conditions.
Package
Container, closure, label, code, finished pack and approved files.
Output
Required rate for a named format, shifts, annual plan and changeovers.
Factory
Measured space, utilities, access, drainage and local site constraints.
Project scope
Equipment boundary, documents, FAT, delivery, startup and destination.
Allot Tech organized recurring buyer questions, project-scoping patterns, available catalog inputs and specialist-resource context into a decision sequence. No customer case, certification, output guarantee or factory ownership is implied unless separately verified for the named project.
Manufacturing context
Use equipment views to ask more specific project questions.
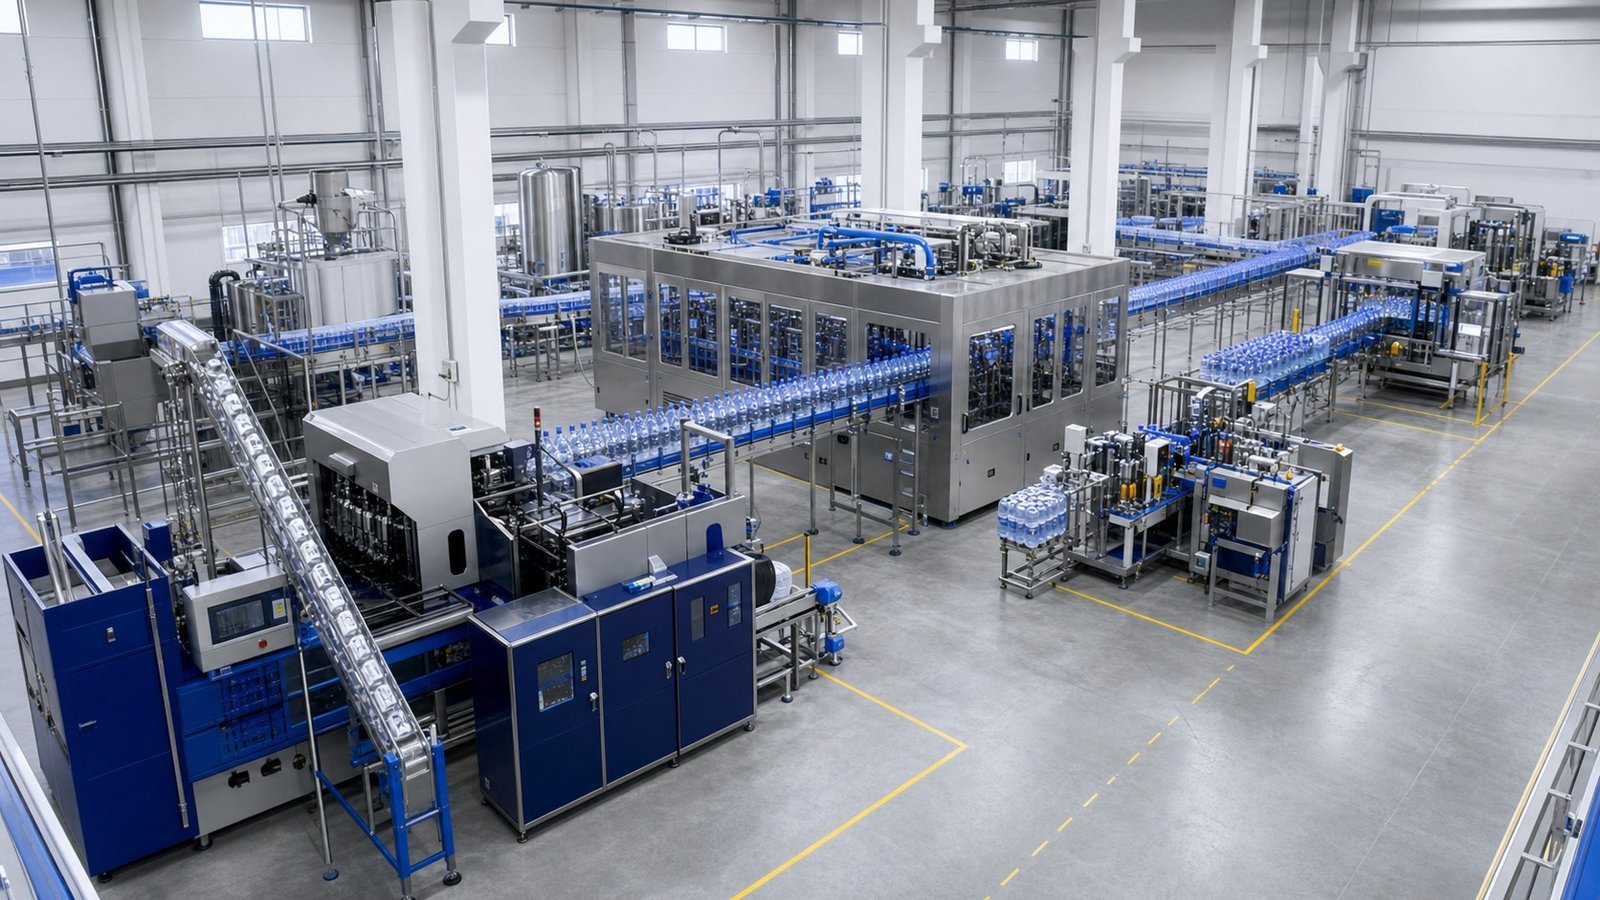
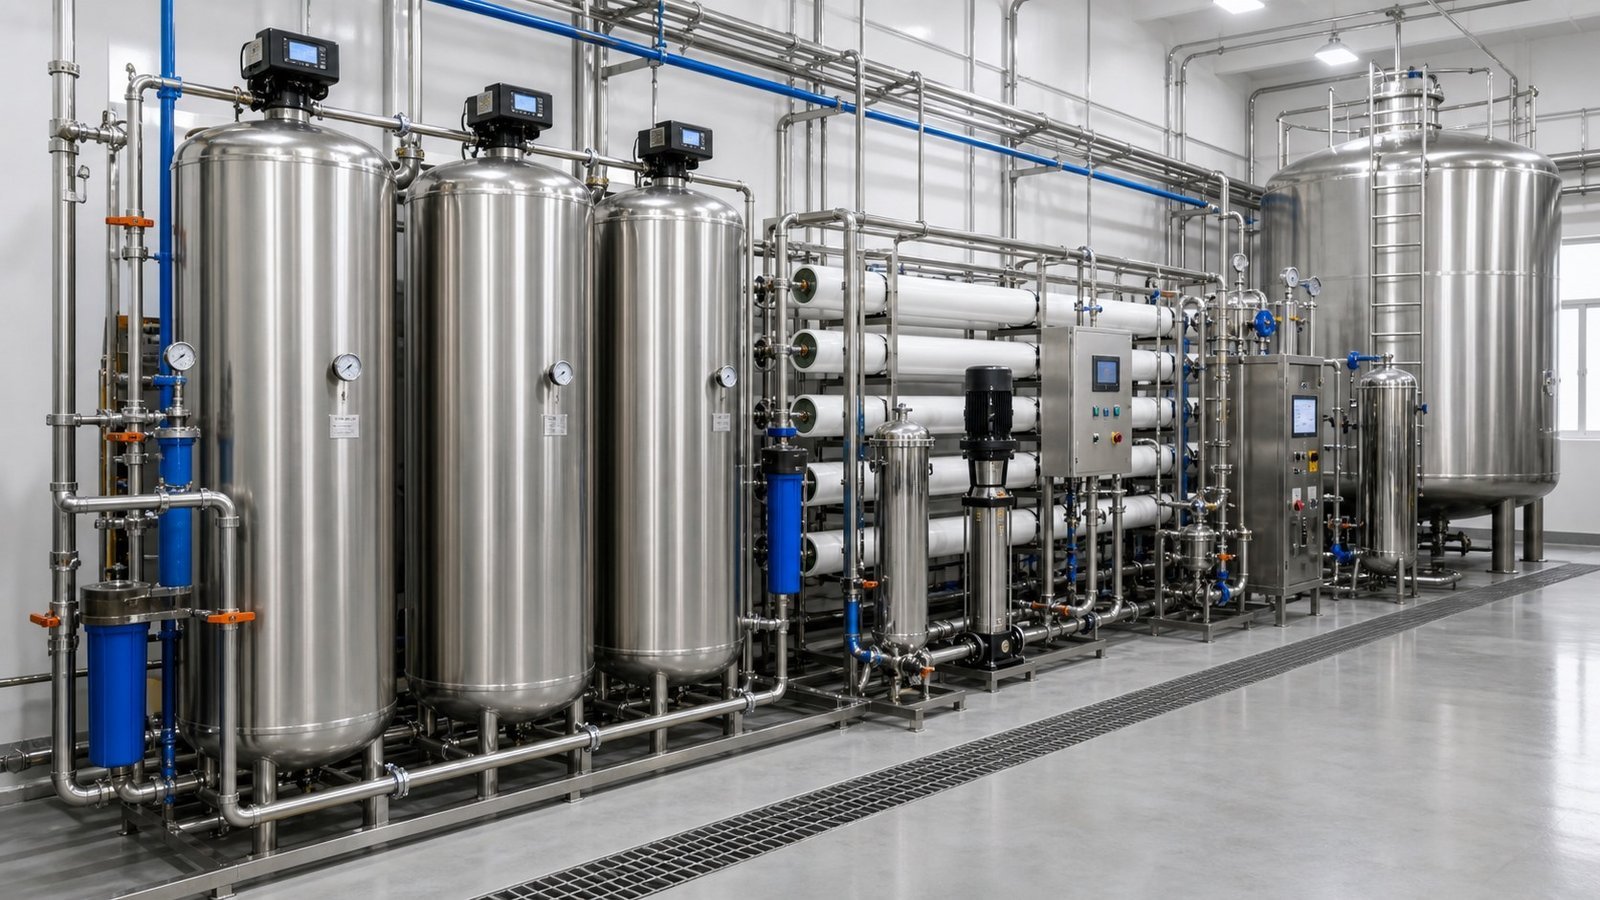
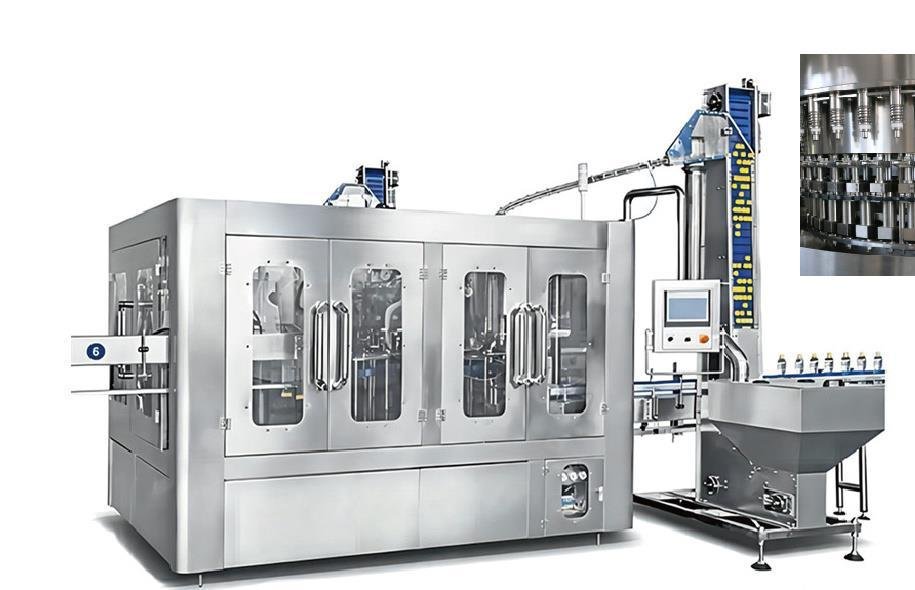
The process illustration supports scope discussion. The XGF equipment image is reproduced from page 9 of the Allot Tech 2026 catalog; use the catalog and project documents to review the applicable configuration.
Buyer questions
Frequently asked questions
What is included in a 5 gallon water filling line?
Typical scope includes bottle receiving, decapping, pre-washing, internal and external washing, rinsing, filling, capping, inspection and optional bagging, conveying or rack handling.
Can the same line handle 3 and 5 gallon bottles?
Some configurations may support both sizes, but bottle dimensions, necks, caps, guides, wash carriers and output must be confirmed with approved samples.
Why does returned-bottle condition matter?
Contamination, damage, odor, old labels and mixed formats affect sorting, washing, rejection rate, hygiene and actual output.
What layout information is important?
Show dirty-bottle receiving, clean production, drainage, chemical area, operator access, finished-bottle storage and dispatch routes.
Project discussion
Discuss a 5 Gallon Water Line
Send the beverage, package files, required output, factory conditions, destination and current project stage.