Beverage quality & acceptance
Bottling Line Site Acceptance Test
Turn the site acceptance test into a documented production trial at the installed factory, with a clear distinction between mechanical readiness and accepted performance.
Published by Allot Tech. Project contact: founder Mr Kcal. Final engineering, performance, materials, compliance, manufacturing responsibility and commercial terms must be confirmed for the selected resource and signed project scope.
Updated September 14, 2026
Direct answer
Acceptance requires a reproducible run boundary.
A bottling line site acceptance test, or SAT, checks the installed system under the agreed site conditions. Define the product and package, utility readiness, staffing, test duration, output counting point, quality checks and stop-classification rules before the run. The plan should also identify safety and installation release responsibilities, unresolved FAT items and the evidence needed for handover. A successful factory test is useful prior evidence but cannot by itself demonstrate operation with the destination factory utilities, interfaces and production materials.
Project definition
Start with the complete decision basis.
Turn the site acceptance test into a documented production trial at the installed factory, with a clear distinction between mechanical readiness and accepted performance.
Accepted basis
Signed scope, approved drawings, FAT record, equipment list, outstanding issues and the installed configuration.
Site readiness
Utility measurements, completed interfaces, access, trained staffing and release by the responsible site specialists.
Test materials
Named beverage or approved test medium, bottles or cans, closures, labels, packs and quantities for the agreed runs.
Test rules
Formats, duration, measurement boundary, exclusions, quality sampling, data ownership and retest triggers.
System or development path
Build a review sequence with named records and decision owners.
Close readiness gaps
Review installation records, utilities, training and open FAT points before scheduling the performance run.
Agree the run sheet
Freeze product, format, speed basis, counting points, sampling and stop classification with both parties.
Record the complete trial
Keep start and end times, good packs, rejects, stop events, process conditions and quality results together.
Sign the disposition
Separate passed items, corrective actions, conditional release and repeat tests with named owners and due dates.
Quotation comparison
Agree the comparison basis before sampling or ordering.
| Decision area | Buyer should provide | Proposal should clarify |
|---|---|---|
| Production boundary | Good output counted at an agreed point. | Definition of filler rate versus finished-pack rate. |
| Test time | Agreed duration and permitted interruptions. | Raw timeline and stated treatment of each stop. |
| Quality | Approved package and product checks. | Traceable results and handling of suspect production. |
| Handover | Documents, training, spares and unresolved items. | Signed acceptance record and responsibility for closure. |
Buyer working matrix
Acceptance requires a reproducible run boundary.
Use the matrix to prepare the SAT document with the responsible buyer and supplier.
| Requirement | Evidence | Disposition |
|---|---|---|
| Site readiness | Released installation and utility records | Ready or action required |
| Output | Time, counting point, good output and event log | Compared with the signed test basis |
| Quality | Product and package sampling records | Released, held or corrective action |
| Handover | Manuals, backups, training and open-item list | Accepted or assigned for closure |
Solve the next project problem
Close these proposal gaps before price becomes the decision.
Use the brief below to turn a vague supplier conversation into questions that can be answered and documented.
Make this decision comparable.
Send: Good output counted at an agreed point.
Require: Definition of filler rate versus finished-pack rate.
Make this decision comparable.
Send: Agreed duration and permitted interruptions.
Require: Raw timeline and stated treatment of each stop.
Make this decision comparable.
Send: Approved package and product checks.
Require: Traceable results and handling of suspect production.
Send the beverage, package files, required output, factory conditions, destination and current project stage. The Allot Tech Project Desk can help organize the first comparison.
Decision evidence
Keep project evidence connected to each approval and release decision.
Evidence should be identified before the order or approval stage so both sides know what will support the next decision.
Approved engineering basis
Keep the signed specification, equipment list, package files, layout and interface responsibilities under revision control.
Manufacturing progress record
Identify agreed drawings, component confirmations, photographs, open questions and approval decisions by date.
Test and acceptance record
State configuration, materials, operating conditions, measurements, results, punch-list items and release status.
Delivery and handover package
Connect packing, serial numbers, manuals, backups, spare parts, training and support contacts to the delivered scope.
Separate commissioning from contractual acceptance
Commissioning involves adjustment, debugging and operator familiarization. SAT is a pre-agreed evaluation with defined evidence. A line running during commissioning does not automatically mean all purchase requirements have passed. Prepare the SAT document before the visit so the supplier and buyer can plan materials, instruments and decision-maker availability.
- Use a distinct acceptance run identifier
- Retain commissioning changes
- Agree who may sign each requirement
Use one event timeline for output and stops
If the filler counter and packer count disagree, record where rejects, samples and work in progress sit. State whether output is containers or saleable packs. Classify a starved filler, label stoppage, utility interruption and planned sample stop consistently; do not remove inconvenient events after the result is known.
- Record counter positions
- Reconcile rejects and retained samples
- Agree exclusions before the run
Make a punch list usable after the supplier leaves
Each open item needs a requirement reference, evidence, owner, corrective action, due date and verification method. Distinguish missing documentation from a failed performance requirement. Record whether an item prevents production, prevents final acceptance or can be closed during an agreed follow-up. These are project decisions for the named approvers, not assumptions hidden in the report.
- Attach photos or logs to each finding
- Name the verification owner
- Keep the final handover revision
Decision gates
Move forward when the next commitment has enough written evidence.
Project stages overlap, but each commercial commitment should have a visible basis, named approvers and a list of unresolved items.
Engineering basis approved
The product, package, output, equipment boundary, layout, utilities, responsibilities and open assumptions are controlled.
Manufacturing and test basis approved
Drawings, component schedule, test materials, acceptance conditions, documents and planned evidence are agreed.
Delivery and handover released
Punch-list closure, packing, shipment files, site readiness, installation scope, training and support ownership are visible.
Before requesting a proposal
Build one brief that every resource can answer on the same basis.
This page is designed to help an international buyer prepare a clearer discussion, not to replace the responsible resource’s engineering or the buyer’s professional review.
Product
Beverage, process, hygiene, shelf-life and operating conditions.
Package
Container, closure, label, code, finished pack and approved files.
Output
Required rate for a named format, shifts, annual plan and changeovers.
Factory
Measured space, utilities, access, drainage and local site constraints.
Project scope
Equipment boundary, documents, FAT, delivery, startup and destination.
Allot Tech organized recurring buyer questions, project-scoping patterns, available catalog inputs and specialist-resource context into a decision sequence. No customer case, certification, output guarantee or factory ownership is implied unless separately verified for the named project.
Reference basis
Primary and specialist sources used to frame the buyer questions.
These sources support definitions and planning context. The current edition, local requirements and project-specific acceptance criteria still need confirmation by the responsible parties.
- Krones: Canning line installation and acceptance
A manufacturer case distinguishes arrival, commissioning and whole-line acceptance. It is external industry context, not an Allot Tech customer claim.
Manufacturing context
Use equipment views to ask more specific project questions.
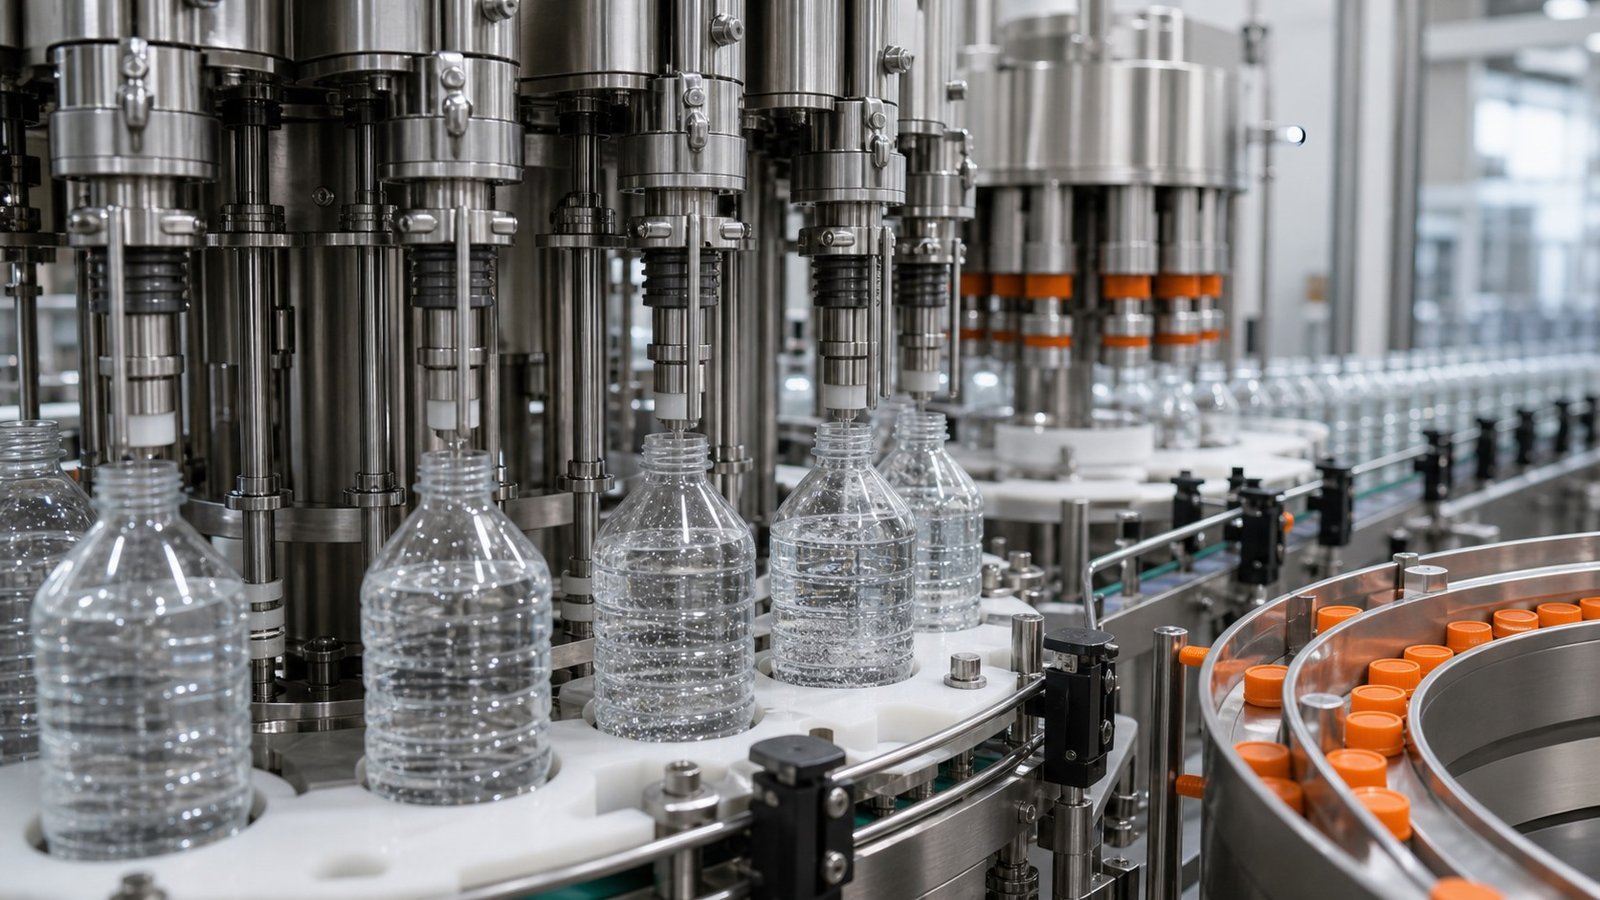
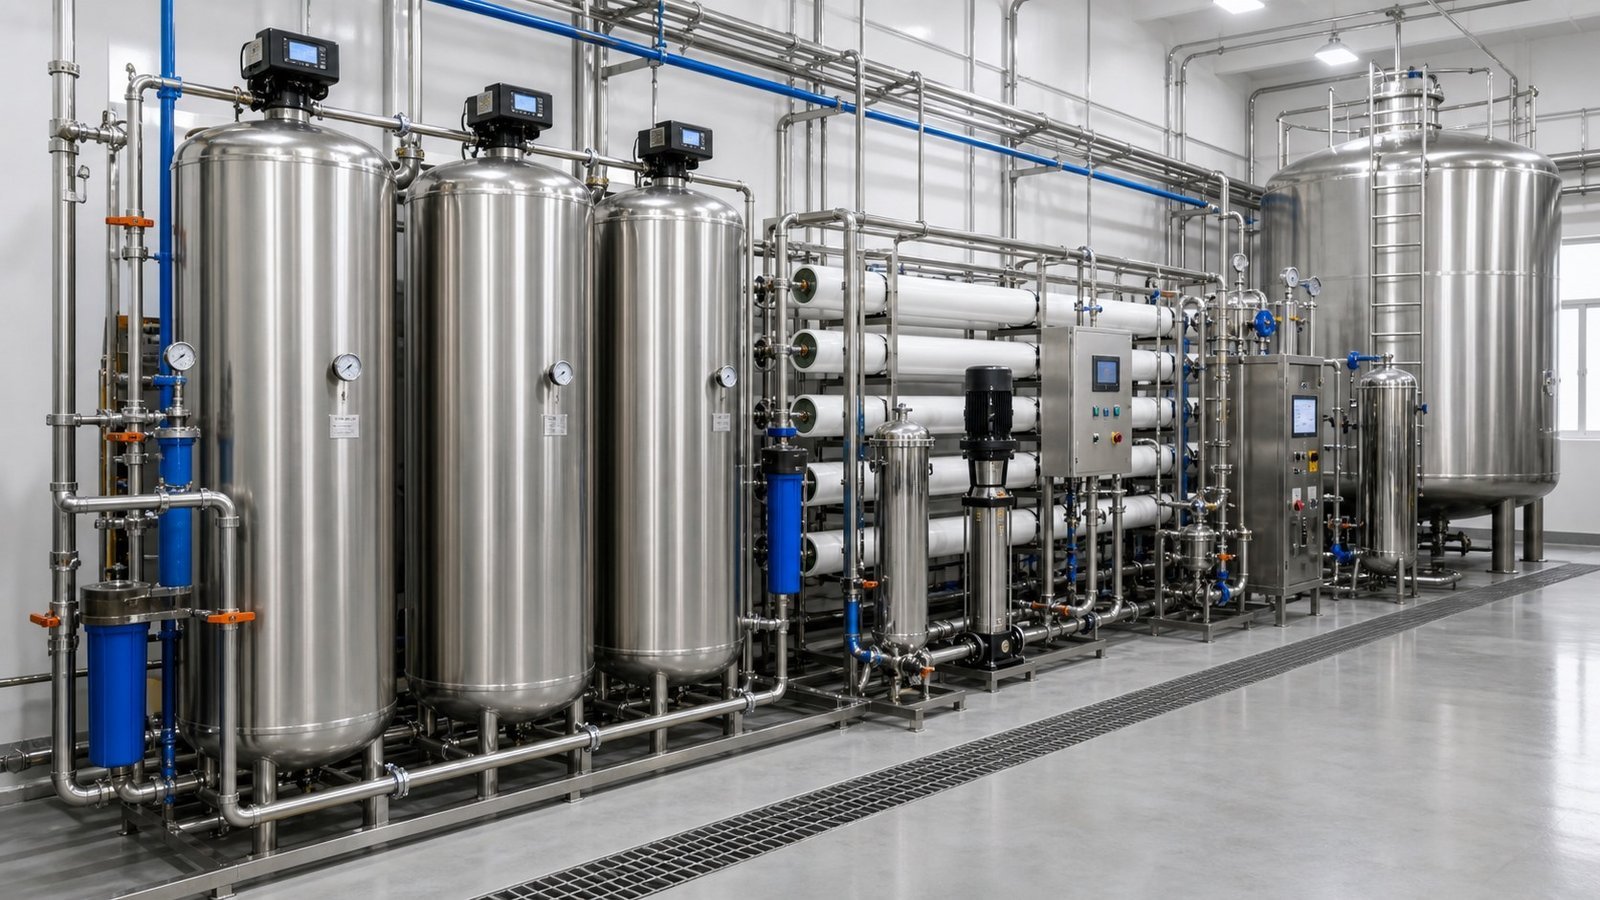
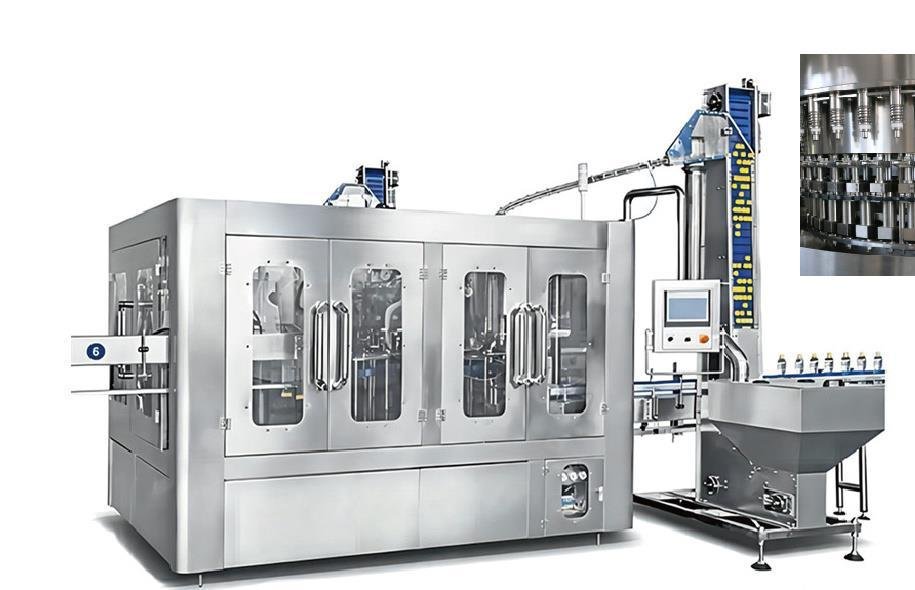
The process illustration supports scope discussion. The XGF equipment image is reproduced from page 9 of the Allot Tech 2026 catalog; use the catalog and project documents to review the applicable configuration.
Buyer questions
Frequently asked questions
How is SAT different from FAT?
FAT occurs before shipment at the supplier location. SAT evaluates the installed system at the destination under agreed site conditions. The two records should connect but have different boundaries.
Should every bottle size be tested?
The purchase specification should identify which formats require acceptance runs and which changes are covered by other evidence. Do not assume one format proves all formats.
Can a punch list remain open after the run?
Only with an explicit disposition from the authorized parties, including the effect on release, responsibilities and how closure will be verified.
Project discussion
Discuss This Beverage Project
Send the beverage, package files, required output, factory conditions, destination and current project stage.